Robotic collate-and-load for snack sticks, sausages and string cheese

From bulk bin to consistent, repeatable rows,
in one system.

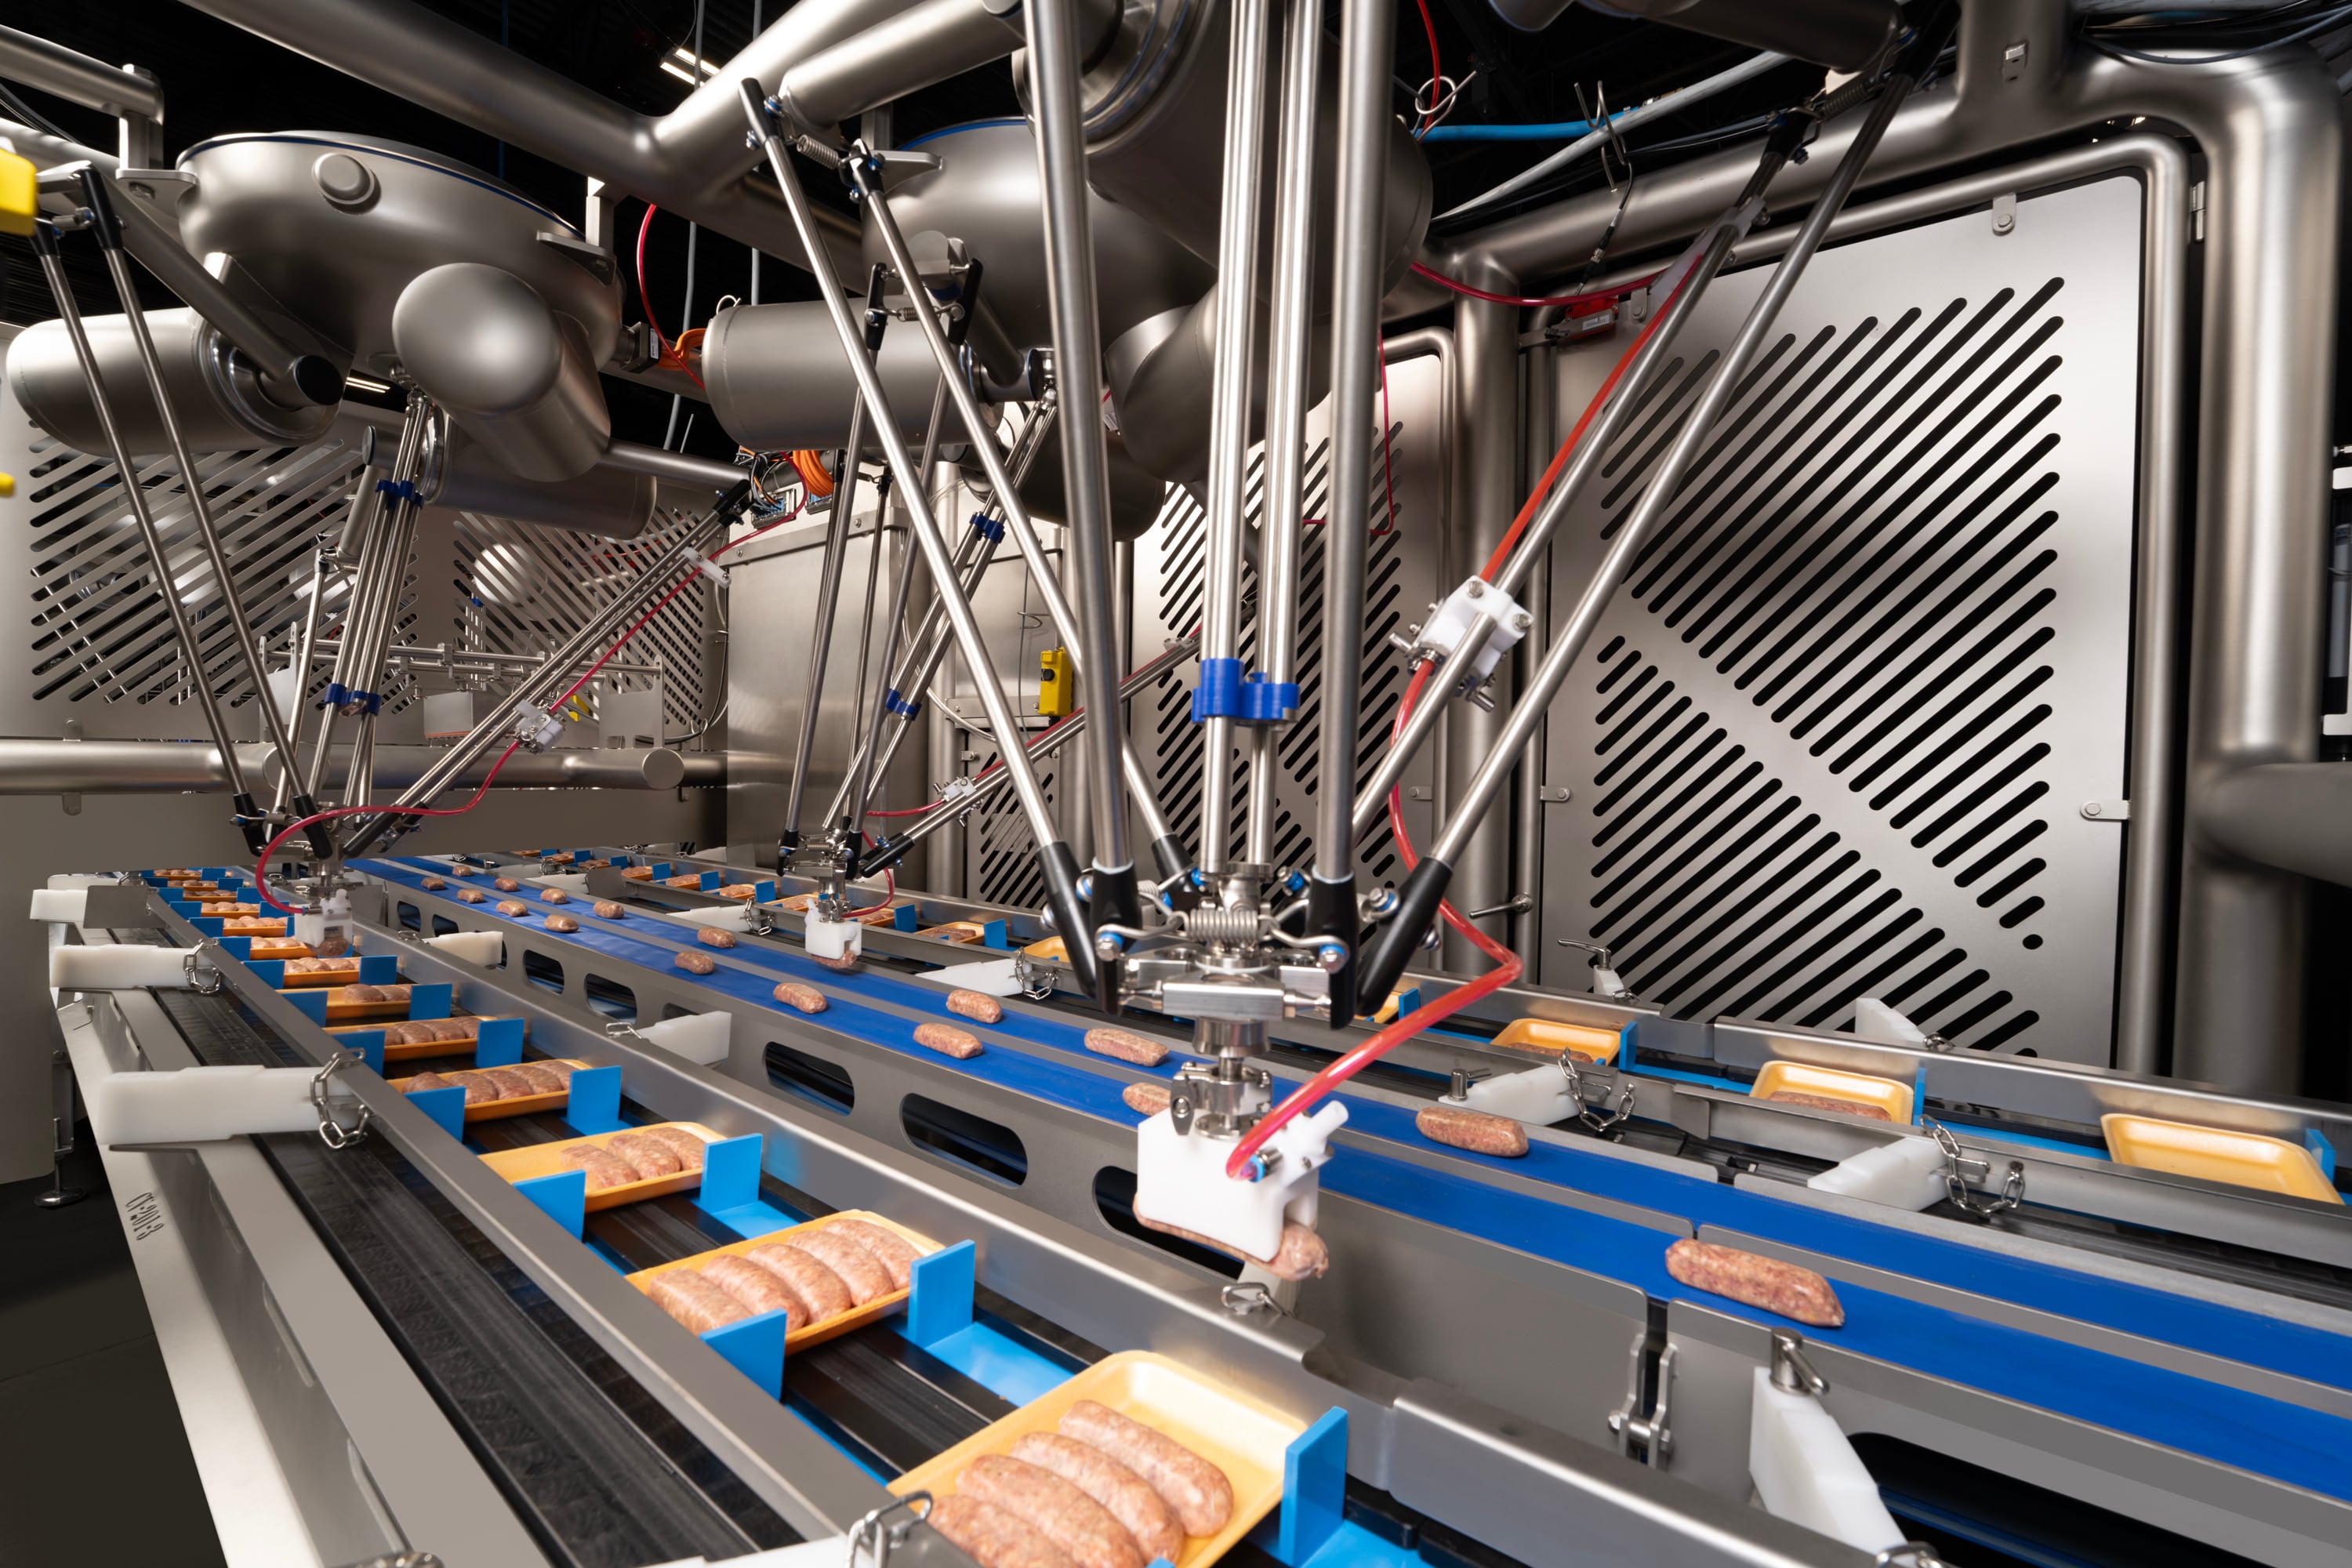
The Kestrel takes cylindrical food products — snack sticks, straight sausages, hot dogs, string cheese — through singulation, collation, and robotic loading into thermoformer pockets: centrifugal feeding, collation, and robotic loading in one system. A small stylist crew stays on the line for product presentation — the heavy, repetitive labor is automated. Compact footprint. Built for washdown protein environments.
Centrifugal
High-speed Singulation
Gang-Pick
Washdown-Rated Delta Robot
Compact
Small-footprint Design
Washdown
Rated Construction
Multiple PatentsAll in Food Packaging Automation
In-House ProgrammingControls, Vision & Robotics Expertise
Factory-Tested ReliabilityBacked by JLS Service & Support
Installation & SupportDedicated Installation, Startup & Support Team
Delivery Timeline at ProposalTarget delivery scoped to your project
JLS Kestrel watercolor bird illustration

The JLS Kestrel is a robotic collate-and-load system for uniform cylindrical food products — snack sticks, straight sausages, hot dogs, and string cheese. High-speed centrifugal singulation moves product from bulk to single-file presentation, a custom collation conveyor aligns it into rows, and a washdown-capable delta robot gang-picks multiple items per cycle into thermoformer pockets. Compact footprint, washdown-capable construction, minimal manual handling — a small stylist crew remains for product presentation.
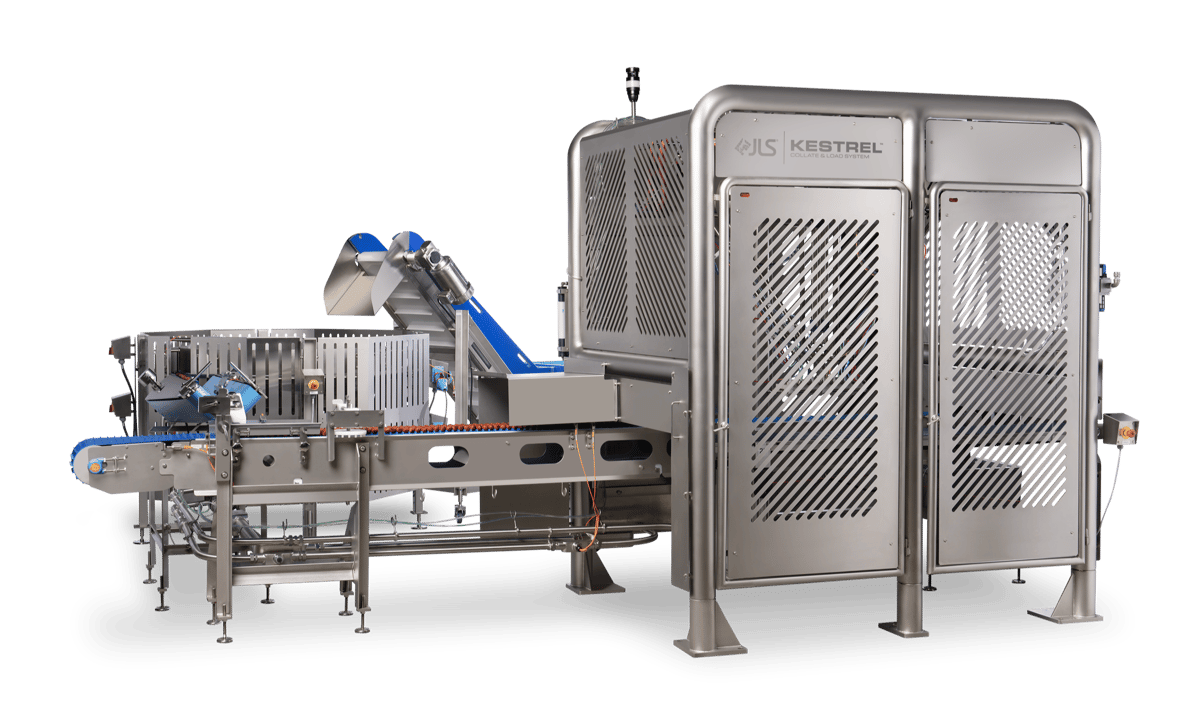
JLS Kestrel washdown-ready collate-and-load system for cylindrical protein products such as snack sticks and straight sausages

In action

Watch the Kestrel collate and load —
at line speed.

The Kestrel collating and loading stick-format product — centrifugal feeding, collation, and loading in one system.

Why Kestrel

Bulk to package. Minimal touchpoints.

Snack sticks, sausages, and hot dogs are among the hardest products to handle at speed — cylindrical, variable, quick to roll, and often moisture-affected, arriving from bulk in no particular order. Manual singulation and loading are repetitive, hard to staff, and inconsistent. The Kestrel was built to close that gap, taking product from random bulk to accurately collated rows to loaded thermoformer pockets in one continuous, coordinated system.

Random bulk in. Precise placement out. Every Kestrel is configured to your exact product diameter, length, and pack count — so the most physically demanding job on the protein line becomes one of the most reliable.

Applications & Pack Formats

The Kestrel —
washdown-ready collate and load.

Designed for uniform cylindrical food products — snack sticks, straight sausages, hot dogs, string cheese. Single-file describes how product is presented to the cell; gang-pick means the tooling picks multiple products in one robot cycle, normally placing one product per pocket. Head count — single or dual — is selected during system design to match your rate.

Products Handled

Meat snack sticksBeef, pork, turkey, blends
Straight sausagesFresh, smoked, cooked
Hot dogsSingle or multi-pack
String cheeseUniform stick formats
Other cylindrical productTalk to our engineers

Pack Formats & Configurations

Single-file presentationHow product reaches the cell
Gang-pick toolingMultiple products per robot cycle
Single-head robotSelected at system design
Dual-head robotHigher rates, chosen at design
Thermoformer infeedDirect pocket placement

Primary Product Handling

KestrelYou’re here
TalonFlow wrap, thermoform, tray load
HarrierBacon draft loading

The Challenge

Hand-loading a thermoformer is the slowest job on the line — and the system built to end it.

✕The Problem

Hand-collating cylindrical product is slow, repetitive — and hard to keep staffed

Rolling product, drifting counts, empty pockets — every shift.

Cylindrical product rolls, counts drift, and pockets run empty when crews fall behind — the thermoformer sets the pace, and manual collation can't hold it shift after shift. Add high turnover in these repetitive roles and rising ergonomic claims, and the cost of doing it by hand keeps climbing.

Chronic
Turnover in manual packing roles
Empty pockets
When manual loading falls behind the former
Line rate
Throughput manual handling can't sustain
✓The Solution

Engineered robotic automation configured to your exact product

JLS engineers, tests, and installs the system — proven before it ships.

JLS designs the system around your product, package, and line — centrifugal feeder, collation conveyor, robot, tooling, and controls engineered and programmed in-house. We validate the application on your actual product during the pre-sale process, then prove the full system at Factory Acceptance Testing before it ships — so the line runs at rate, holds consistent pocket counts every cycle, and stands up to daily washdown.

FAT
Validated in factory testing before shipment
Recipe-driven
Tool-less SKU changeover
In-house
Controls & software, by JLS

Customer Case Study · JLS Kestrel Collate and Load System

From bulk bin to thermoformer pocket — without a manual loading position.

A protein processor needed to automate loading of snack sticks into a thermoformer. Hand-loading required multiple operators per shift and generated inconsistent pocket counts — when workers fell behind, pockets ran empty and rejects climbed. The line needed automation that could match the thermoformer’s continuous pace.

JLS engineered and installed a Kestrel system with centrifugal singulation, a custom collation conveyor, and a gang-pick delta robot. Product moves from bulk infeed through singulation, aligns on the collation conveyor, and is gang-picked directly into thermoformer pockets in consistent counts every cycle. Operators run it from the HMI, automating repetitive loading tasks that have become increasingly difficult to staff.

The automation process is smooth, precise, and highly consistent, allowing our packaging lines to maintain production targets with greater reliability and less downtime.

— Carlos O'Neill, Plant Manager, Family Food Products, Inc.

Get the full case study

See the configuration, throughput, and results behind this install.

Tell us more about your challenge

By submitting, you agree that JLS Automation and Robert Reiser & Co. may contact you about your inquiry.

Questions about this application? Talk to an expert →

Flight Lab

See the Kestrel run your product
before you commit.

JLS Flight Lab runs your application on a robotic feasibility test system in York, PA. Send product samples — or a close proxy, subject to project scope and availability — and JLS application engineers test tooling for your size and pack pattern and confirm the right test method for centrifugal feeding and pocket replication, so feasibility is established before the design is finalized. Rate and performance are validated during the project FAT before shipment, with final commissioning completed at your facility.

Feasibility
Tooling & pick method tested
U.S. Built
U.S. built automation
Pre-sale
Application testing, subject to availability
Test your product in the Flight Lab

Core Technology

The engineering behind the precision.

Every JLS system is engineered, integrated, programmed, and built in York, Pennsylvania on proven industrial robot and control platforms — from centrifugal feeder engineering to custom collation conveyor design to operator-first controls and software. JLS holds multiple patents across its food-handling portfolio, and it shows in the details: application engineering, configured tooling, real-product testing, 1,000+ installations, and U.S.-based support.

Stainless steel construction icon
IP69K*-rated components

Cleanable to washdown construction

Open-channel stainless frame, sloped surfaces, and NEMA 4X-rated control enclosures — offered in cleanable construction for bakery and dry environments, and full sanitary washdown construction for wet protein. Built for the food zone from day one. Not retrofitted.
IP69K*-rated components Minimal Harborage NEMA 4X enclosures
Gang-pick delta robotics
Singulate · Collate · Gang-pick

Washdown-rated gang-pick delta robotics

High-speed centrifugal singulation and a custom collation conveyor present product in aligned rows at pick pitch — so the washdown-rated delta robot gang-picks multiple items per cycle and places them directly into thermoformer pockets, with minimal manual handling.

Gang-pick Centrifugal singulation Collation conveyor
VOB vacuum tooling icon
Mechanical · Vacuum · Gang-Pick

Flexible tooling — mechanical or VOB 2.0

Gang-pick mechanical tooling handles firm cylindrical products like snack sticks and straight sausages; JLS-engineered VOB 2.0 Vacuum on Board tooling handles wet, soft, or irregular product while reducing compressed-air use. Every tool is configured and lab-tested for your exact product.
Mechanical or Vacuum CFD-Optimized Airflow Multiple Patents
Fast tool-less changeover
Built Into VOB 2.0

Fast, tool-less changeover

Select the new recipe on the HMI, swap the end-of-arm tooling by hand, and run. Every purchased, validated SKU is loaded before the system ships; changeover time depends on the application and which components change — EOAT, chutes, bowl-feeder tooling, or collation components.

Recipe-Driven SKU Swap Validated Recipes Loaded
Multi-cell, multi-head modularity
Single · Dual head

Single- or dual-head scaling

Match throughput to your line at system design — a single-head robot for standard rates, or a dual-head configuration when the rate demands it. Head count is an engineering decision made during your project design, sized to product, package, and target rate.

Single or dual head Sized At System Design
In-house programming and HMI icon
York, PA · Designed & Programmed In-House

Operator HMI & in-house software

Touchscreen interface designed for plant-floor operators — select a validated recipe and run — normal production operation doesn’t require an engineer or robot-programming expertise. JLS programs and supports the application controls on commercially available B&R technology, so new recipes and remote support come directly from the team that programmed your system.

In-House Programming ERP/MES Integration Available

Options & Add-Ons

More ways to fit your line.
Integrated sanitary infeed
Integrated Sanitary Infeed
JLS coordinates sanitary infeed conveyors that present product cleanly and consistently to the robots — the steady, even supply that accurate gang-pick placement depends on.
Washdown upgrade icon
Washdown upgrade (IP69K*-rated components)
Add washdown-capable construction with IP69K*-rated components for wet protein environments — specified per application.
Configure Your System
Need Something Specific?
Every Kestrel is configured to your product diameter, length, and pack count. Talk to a JLS application engineer about your exact requirements.
Talk to an Engineer →

Flexible thermoformer integration

Collate and load into the thermoformer already on your floor.

Already have a thermoformer in place? The Kestrel integrates with compatible thermoformers based on application and interface requirements — delivering product at the correct count, pitch, and cycle rate through coordinated mechanical integration and controls communication.

Planning a new line? JLS can coordinate with your thermoformer OEM to support a complete collate-and-load system, with the thermoformer, robot, infeed, and product handling planned together from the start.

Application Engineering & Integration

Configured for your product.
Scalable across your line.

Every Kestrel ships from the same proven platform — configured to your product, count, and pattern, with centrifugal singulation and collation feeding the non-vision delta robot. One team, one facility, one integration.

UPSTREAM Stick / sausage / cheese production KESTREL COLLATE & LOAD CENTRI-SINGULATION PER APPLICATION DOWNSTREAM Thermoformer seal & trim OUTPUT Case packing
JLS + Reiser: Expertise across the line

Planning more than just collation and loading?

JLS delivers complete primary and secondary packaging lines — from bulk infeed through primary loading and case packing — coordinating third-party case erecting, sealing, and load securement as part of one solution.

Full food production line — JLS + Reiser: expertise across the line Ten production-line stages across four zones. JLS-built robotic automation stages are shown in purple; stages available through Reiser's OEM portfolio in blue; customer-selected or partner equipment in gray. Dashed lines mark coordinated integration points. Prepare. Portion. Form. Load. Seal. Case. Carton. Collate. Stack. Secure. 01Mixing &blendingGrindingEmulsifyingMarinatingTumblingAvailable throughReiser portfolio 02Forming &portioningStuffingExtrudingPatty formingDepositingAvailable throughReiser portfolio 03FurtherprocessingSlicingDicingShreddingTenderizingAvailable throughReiser portfolio 04PrimaryloadingPick & placeVision-guidedLane loadingProduct collationJLS TALONJLS KESTRELJLS Automation 05PrimarypackagingThermoformingTray sealingVacuum / MAPSkin packAvailable throughReiser portfolio 06CasepackingRobotic case loadingRobotic loadingWashdown configurationsWashdown optionsJLS OSPREYHAWK · PATTY HAWKCase erecting & sealing via partner equip.JLS Automation 07CartoningForm, load,close cartonsCompact footprintWashdown-capable designJLS PEREGRINEPEREGRINE ISJLS Automation 08Collation /bundlingCount & stackBundle packMultipackPartner equipmentscope-dependent 09PalletizingLayer buildingRobotic palletizingSlip-sheet placeLayer padPartner equipmentscope-dependent 10LoadsecurementStretch wrapBandingCorner boardTop sheetPartner equipmentscope-dependent Tier 1 Primary Packaging The package that touches the product Tier 2 Secondary Packaging Cases, cartons, and multipacks for retail or distribution Tier 3 Tertiary Packaging Stretch wrap, ship-ready unit

Together, JLS and Reiser help food manufacturers develop coordinated processing and packaging lines—from product preparation and primary package loading and sealing through cartoning and case packing, with third-party collation, palletizing, and load securement coordinated into the plan.

Illustrative line architecture. Stages, equipment suppliers and sequence vary by product and project scope. Not every food line uses every stage, and slicing, cooking, freezing, inspection and other processes may occur in different positions.

Scroll left and right to scan the full line. Open the printable line map →

JLS-built robotic automation Available through Reiser’s OEM portfolio Customer-selected / third-party equipment Coordinated integration point

Reiser role across the line

Food-processing expertise, application development, equipment selection, product testing, and sales & lifecycle support.

JLS role at robotic packaging stages

Robotic engineering, product & package handling, controls interfaces, and integration & FAT when included in project scope.

Let’s talk more about planning your full line.

Tell us who you are and a bit about your line. An automation expert will reach out — and we’ll bring the right people from JLS and Reiser to the conversation.

Your details
Facility location
Your line today
What you're planning
What solution(s) are you interested in?* Select all that apply.
Project timeline

By submitting, you agree that JLS Automation and Robert Reiser & Co. may contact you about your inquiry.

The automation process is smooth, precise, and highly consistent, allowing our packaging lines to maintain production targets with greater reliability and less downtime.
Carlos O'Neill, Plant Manager Family Food Products · JLS Kestrel Collate and Load System

Specs & Configuration

Kestrel technical specifications.

Configuration snapshot

Kestrel is available in single-head and dual-head configurations. Throughput depends on product diameter, pack count, and target rate — JLS confirms the right configuration during a line assessment.

Single head
Up to 600 ppm (single head)*
*Depends on product and package type.
Standard-rate applications and compact footprint.
Dual head
Scales beyond single-head rate*
Higher-rate applications requiring greater capacity.

*Throughput varies by product, pack count, and configuration. Contact JLS for your specific application.

Specification Value
System type Centrifugal singulation + collation conveyor + washdown-rated delta robot
Products handled Uniform cylindrical products: meat snack sticks, straight sausages, hot dogs, string cheese
Robot type Delta robot (4-axis)
Pick method Gang-pick — multiple items per cycle
Throughput Up to 600 ppm (single head)*; multi-head configurations scale beyond — final rate depends on product and package type*
Configurations Single head; dual head (higher throughput)
Product size range Confirmed during the proposal process — depends on product diameter, length, and package type.
End-of-arm tooling Actuated VOB vacuum tooling (multi-pocket loading)
Approximate footprint (excl. tunnel guards) Confirmed during the proposal process — depends on configuration (single- or dual-head).
Construction levels Full sanitary washdown construction
Infeed method High-speed centrifugal singulation
Collation Custom collation conveyor — aligns product into rows at pick pitch
Target application Thermoformer pocket loading (direct placement)
Washdown construction IP69K-rated components; washdown construction
Frame construction Open-channel stainless frame; minimal harborage points
Control system B&R Automation
Electrical supply 480V ±10%, 3-phase, 60Hz
Air supply 80 PSI, clean, dry, lube-free
Electrical enclosures NEMA 4X rated; UL/cUL listed
Built York, PA — engineered, programmed, and tested in-house by JLS

*Throughput varies by product diameter, pack count, and configuration. Specifications may vary — contact JLS for your specific application.

Where should we send it?

What solution(s) are you interested in? (optional) Select all that apply.

By submitting, you agree that JLS Automation and Robert Reiser & Co. may contact you about your inquiry.

Compare

Kestrel vs. the field.

Feature Manual loading Belt-and-rail singulation Kestrel
Singulation method Operator by hand Belt and rail guide Centrifugal — no product contact pinch points
Throughput consistency Variable — depends on operator pace and fatigue Moderate; sensitive to product size variation Consistent — automated cycle, every shift
Gang-pick loading Manual — tedious, prone to count errors Typically single-file only Delta robot gang-picks multiple items per cycle
Washdown capability N/A Varies; often limited Washdown construction; IP69K-rated components
Footprint Depends on line staffing Can be long / complex Compact — centrifugal feeder + short collation conveyor
Labor requirement Multiple operators per shift Reduced but still requires monitoring No manual loading position — stylist crew remains for product presentation
Product changeover Immediate but inconsistent Rail adjustment required Recipe-driven HMI; tooling swap for size changes
Integration N/A Upstream only — separate loading step Singulation + collation + loading in one system

Kestrel — frequently asked questions.

Answers to common questions about automating your food packaging line.

The Kestrel is designed for uniform cylindrical food products: meat snack sticks, straight sausages, hot dogs, and string cheese. Products should be consistent in diameter and length — the centrifugal singulation and custom collation conveyor are configured to your exact product dimensions. Contact JLS to confirm suitability for your specific product.

The Kestrel uses a high-speed centrifugal feeder to separate product from a bulk infeed into a single-file stream. Centrifugal singulation is gentler than belt-and-rail methods for cylindrical products and The feeder and collation conveyor organize product for robotic loading; a small stylist crew remains for product presentation.

Gang-pick means the delta robot picks multiple products simultaneously in one cycle rather than one at a time. For cylindrical products like snack sticks, gang-pick tooling picks multiple products in one robot cycle, normally placing one product into each thermoformer pocket. The loading pattern is configured to the product and package — improving throughput and reducing the number of pick cycles required.

The Kestrel is primarily designed for direct loading into thermoformer pockets. JLS application engineers configure the collation conveyor pitch and robot tooling to match your specific thermoformer pocket geometry and product count. Contact JLS to discuss your packaging format.

The Kestrel runs at up to 600 products per minute in a single-head configuration, depending on product and package type. Final rate depends on product diameter, length, pack count per pocket, and head count — single or dual, selected during system design. JLS confirms the right configuration and expected rates during a line assessment using your specific product parameters.

The Kestrel uses IP69K-rated components and is built for washdown protein environments. System-level ingress protection varies by configuration. Contact your JLS representative for full details on the construction level appropriate for your facility and sanitation protocol.

The Kestrel is built with an open-channel stainless frame and washdown construction for protein environments. The open-channel design keeps surfaces visible and accessible so operators can reach all areas during daily sanitation. Tooling changes are designed to be fast and tool-less where applicable.

The Kestrel does not rely on vision guidance the way a pick-and-place robot does. The centrifugal feeder and custom collation conveyor orient and align product mechanically before the delta robot picks. This simplifies the system and reduces sensitivity to product color or surface variation that can affect vision-based systems.

The Kestrel is configured for your specific product diameter and length. Changeover between SKUs that differ significantly in size typically requires a tooling swap and conveyor adjustment. JLS application engineers size the system for your product mix during the design phase.

Changeover time depends on the degree of difference between SKUs. Recipe-driven HMI selections handle parameter changes, while physical tooling swaps are designed to be fast. JLS confirms changeover procedures for your product mix during application engineering.

Often, yes. JLS Flight Lab can test product samples, or a close proxy, subject to project scope and availability, on a robotic feasibility test system with tooling configured for the application. Pre-sale testing establishes feasibility — tooling for your product dimensions and pack pattern, and the right test method for centrifugal feeding and pocket replication — before the design is finalized, reducing project risk. Rate and performance are validated during FAT before shipment, with final commissioning completed at your facility.

The Kestrel is engineered, programmed, and tested entirely at JLS Automation's facility in York, Pennsylvania. JLS handles design, controls programming, Factory Acceptance Testing, and ongoing service in-house — with remote diagnostics and direct access to JLS engineering and programming expertise.

To scope a Kestrel, JLS typically reviews your product type, dimensions (diameter and length), target throughput, pack count per pocket, thermoformer model, sanitation requirements, available floor space, and the production problem you need to solve. Clear application detail up front allows JLS to recommend the right configuration and estimate scope accurately.

Still have a question that isn’t answered here?

What do you want to know?

Ask us anything — an automation expert will follow up.

What can we help with? Optional — select any that apply.

By submitting, you agree that JLS Automation and Robert Reiser & Co. may contact you about your inquiry.

Talk to an automation expert

Have sticks, sausages, or string cheese you need loaded?

Tell us about the product, the package, and what you’re trying to automate. A few sentences is enough.

Prefer to talk? Call (717) 505-3800.

By submitting, you agree that JLS Automation may contact you about your inquiry. See our privacy policy.

* Specific components of the Kestrel are IP69K-rated. System-level ingress protection varies by configuration. Contact your JLS representative for full details on your application.

Find out what the Kestrel can do for your line.

We evaluate your product, your thermoformer, and your facility — then show you what will work, what the configuration looks like, and outline the expected payback range for your line — typically 24–36 months, depending on the application. Less guesswork. No force-fitting.

Over 1,000 installations. Predictable, fast performance. Premier, dedicated service.

  • Fast response times (remote + on-site)
  • Experienced JLS technicians
  • Spare parts & lifecycle support
  • Training that sticks with your operators
Have a product you need loaded, packed or cartoned?
Start with whether it’s a fit — not with a quote.
Tell an application engineer what you’re packaging and what the line looks like today. A few sentences is enough. If the product suits it, JLS can test it in the Flight Lab before any design is finalized.
Already running a JLS line?
Connect with the service experts who keep your automation performing.
Spare parts, preventive maintenance, retooling, training, and on-site support — from JLS's in-house support team, backed by direct access to JLS engineering and controls expertise.